 Facebook
 Google
 GitHub
 Linkedin
Why a Conforming Two-Layer ESD Mat Can Fail Incoming Inspection
A shipment read non-conforming until the inspector realized which layer he had measured. Two-layer ESD matting carries two separate resistance specifications, not one.
Last September, we shipped a batch of ESD bench matting to a customer in Southeast Asia. Before it left the factory, we ran our normal outgoing inspection: surface resistance on the green working face, resistance on the black base layer, resistance to ground, thickness, appearance, and packaging. Everything was checked, and the records were filed.
When the material arrived, the inspector measured the other side—the black conductive layer. He obtained a reading of 104 ohms and reported the matting as non-conforming.I knew immediately which side he had measured.
Readings from the same batch cannot differ by two orders of magnitude between our line and his. I asked him to send photographs of the test. When they arrived, the pictures made it clear: the surface resistance meter was sitting on the black conductive layer. That is why it read 104 ohms.
Two Specifications, One Reading
There is nothing strange about the inspector measuring the black side. It is one of the two faces of the mat, and turning the material over during incoming inspection is a normal step.
The two layers do different jobs. The top layer is static-dissipative and controls how quickly charge leaves the working surface. The bottom layer is conductive and moves that charge to the grounding point. Each layer carries its own resistance specification. The two orders of magnitude difference between them is by design, not a defect.
Our cartons carry the specification for both layers. This was a custom order: the base layer was made to the customer's requirement of 103 to 105 ohms, an order of magnitude below our standard 104 to 106 ohm base. Their reasoning was that a more conductive ground layer moves charge away faster. We can build that, but it has a consequence. The base layer now reads even lower, moving further from the working-surface range. If the wrong specification is applied during inspection, the chance of a false failure goes up rather than down.
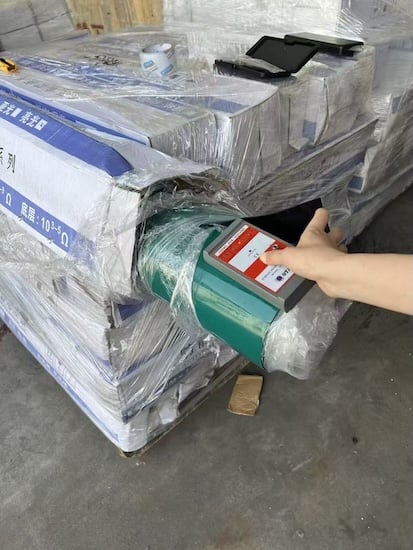
The carton carries the specification for both layers, dissipative surface and conductive base, while the meter sits on the black side. Image used courtesy of ESDBEST
So when he read 104 ohms, the result was conforming to the base-layer specification printed on the carton. However, against the “working surface: 106 to 109 ohms” line on his acceptance sheet, it failed.
The same reading passes or fails depending on which specification you compare it against. The correct specification was printed on the box he had just opened.
Once we walked the customer through the two-layer specification, they re-measured both the green working surface and the black base layer. They confirmed that the material was conforming. They were open about the situation, admitting they were unfamiliar with how the product is constructed, and asked to learn more about static control. Our working relationship has been better ever since.
What I learned from this experience is that making a product well is only half the job. Explaining it clearly is the other half. As the manufacturer, we understand our material better than anyone. However, that understanding does little good if it stays inside the factory.
What We Measure Before a Roll Leaves the Factory
Every batch, and every roll within it, goes through the same outgoing inspection:
- Resistance — measured on both the green working face and the black conductive layer
- Overall thickness
- Layer thickness — the green layer and the black layer measured separately
- Appearance and packaging — wrapped in film, then boxed
A test record is produced for every roll and kept on file.
The first point is worth emphasizing: both faces are measured. We never release a batch based on a single-sided measurement. Because the material carries two specifications, a single reading gives you only half the information.
The same holds in reverse. An inspector who measures only one side also receives just half the information. Which half they get depends entirely on which face was turned up first.
The third point is the one most often skipped. Layer thickness determines the electrical behavior of each layer as well as how much working surface is available to wear through. We measure with a digital caliper at a cut cross-section rather than at a lifted edge. Rubber stretches when peeled back, which shifts the reading. On a 2.0 mm two-layer mat, we measure the green dissipative layer at 0.51 mm and the black conductive layer at 1.55 mm.
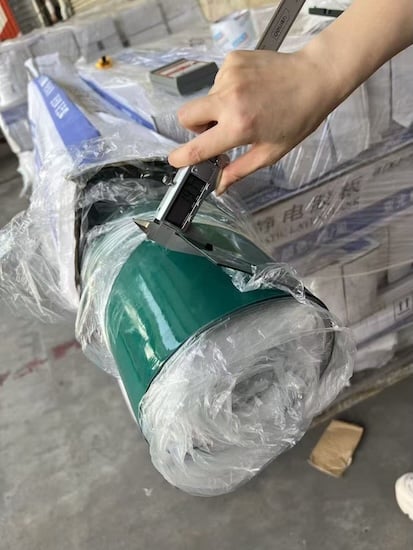
Outgoing inspection: layer thickness measured with a digital caliper before the roll is packed. Image used courtesy of ESDBEST
What Customers Actually Ask About
In practice, the question customers ask most often is not about resistance, which is already listed on the datasheet. What they want to know is how long the mat will last, how well it stands up to abrasion, and whether it will stay clean.
As the manufacturer, we state that the service life for rubber ESD matting is eight to ten years. However, that figure comes with a condition: it depends heavily on how the mat is used and cleaned.
Resistance is not a fixed value; it drifts with wear and contamination. A mat that has been in service for several years, scored by solder debris and wiped down repeatedly, will not necessarily yield the same reading it had when leaving the factory.
Cleaning matters more than most people expect. Industrial alcohol does not dissolve rubber, but it extracts substances from it by leaching out plasticizers and antistatic additives. As plasticizers leach out, the surface hardens. As antistatic additives wash away, the surface resistance drifts upward. Consequently, the mat may look fine even though it is no longer within specification.
This is why acceptance testing cannot be a one-time event. Test the mat upon installation, and then re-test it at the intervals specified by your ESD control program.
Measured Data
The following are point-to-point (PTP) resistance measurements taken on a two-layer rubber bench mat sample. Each layer was measured separately and evaluated against its own range.
Test Conditions
- Instrument: ACL Staticide Model 800 environment and megohmmeter
- Method: point-to-point (PTP), two external weighted electrodes
- Test voltage: 10 V
- Electrode spacing: 150 mm
- Temperature: 29.2–29.4 °C
- Relative humidity: 81.7–82.5 %RH
- Sample: 250 × 300 mm, 2.0 mm two-layer rubber bench mat
- Date: 29 July 2026
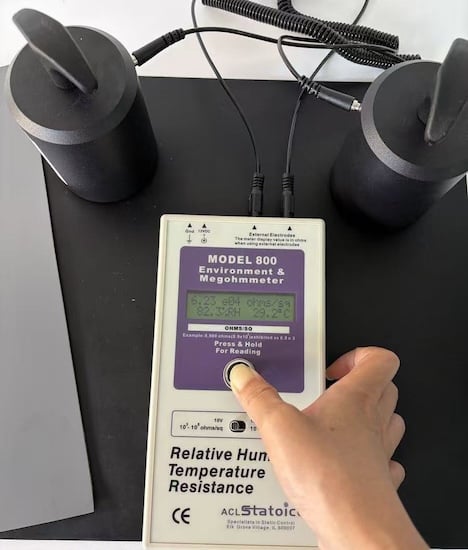
PTP measurement on the black conductive layer: 6.23 × 10⁴ ohms at 82.3 %RH, 29.2 °C. Image used courtesy of ESDBEST
Green dissipative layer — specified 1×10⁶ to 1×10⁹ ohms
| ID | Measured PTP resistance |
| PTP-T01 | 2.00 × 10⁶ ohms |
| PTP-T02 | 2.01 × 10⁶ ohms |
Black conductive layer — standard specification 1×10⁴ to 1×10⁶ ohms
| ID | Measured PTP resistance |
| PTP-B01 | 5.76 × 10⁴ ohms |
| PTP-B02 | 3.12 × 10⁵ ohms |
| PTP-B03 | 3.12 × 10⁵ ohms |
| PTP-B04 | 6.23 × 10⁴ ohms |
| PTP-B05 | 6.26 × 10⁴ ohms |
| PTP-B06 | 3.50 × 10⁴ ohms |
All eight readings fall within the specified range for the layer being measured.
Note how these results must be reported. A statement of the form “8/8 passed 106 to 109 ohms” would be wrong — six of these readings sit below 106 ohms by design. Layer-specific measurements have to be reported layer by layer. Collapsing them into a single pass rate reintroduces the exact error this article describes.
This data represents one sample from one batch, with one measurement per point and recorded ambient conditions. It is not a substitute for lot-by-lot QC records. Surface resistance varies with humidity, which is why conditions are logged alongside every reading. A value quoted without ambient conditions cannot be compared accurately against measurements taken elsewhere.
The Design Is There to Be Understood
Back to that batch bound for Southeast Asia.
Nothing was lost in the end, but the situation clarified an important point for me. The two-layer construction exists to make the product perform better for the user. The dissipative layer protects the working surface, while the conductive layer channels charge to ground quickly. Each layer fulfills its distinct purpose to serve electronics manufacturing. However, a good design only performs well if the people using it understand how it works.
After thirty years of manufacturing this material, the key takeaway remains the same: static control is not just about buying the right product. It is about understanding why the product works the way it does. A mat has two layers, and those layers carry two separate specifications. Recognizing this—and asking “Which layer am I measuring?” before using the meter—prevents the problem entirely.
Manufacturers understand these details, but users do not always. Communicating them clearly is an essential part of our job.